Transforming Modern Industry Through Smarter Digital Solutions
Modern businesses operate in an environment where efficiency, accuracy, visibility, and adaptability have become essential for sustainable growth. Manufacturers and food-related organizations, in particular, manage complex processes involving production planning, inventory, procurement, logistics, quality control, and customer expectations. As these operations become increasingly connected, technology has become a central part of improving performance and maintaining competitiveness. Digital platforms can help organizations reduce manual work, organize information, improve communication, and make informed decisions based on reliable data. Lynqcore Solutions focuses on supporting businesses with technology-driven approaches that can simplify complicated operational processes and create stronger foundations for long-term development.
Manufacturing Software Solutions are becoming an important part of the digital transformation taking place across industrial organizations. Traditional manufacturing environments often depend on spreadsheets, disconnected systems, paper-based records, and manual communication between departments. These methods can make it difficult to maintain accurate information and respond quickly when production requirements change. Modern software can bring important operational functions together within a connected environment, allowing businesses to manage production schedules, materials, inventory, orders, workforce activities, and reporting more efficiently. By centralizing operational information, organizations can gain better visibility into their processes while reducing unnecessary duplication and improving coordination between teams.
The value of digital manufacturing technology extends beyond simply replacing paperwork with software. A well-designed solution can help businesses understand how resources are being used, identify delays, monitor production performance, and recognize areas where processes can be improved. Real-time or regularly updated information can support faster decision-making, especially when production schedules, customer requirements, or material availability change unexpectedly. Automated workflows can also reduce repetitive administrative tasks, giving employees more time to focus on activities that require experience, judgment, and problem-solving. Over time, these improvements can contribute to stronger productivity, better operational control, and more consistent business performance.
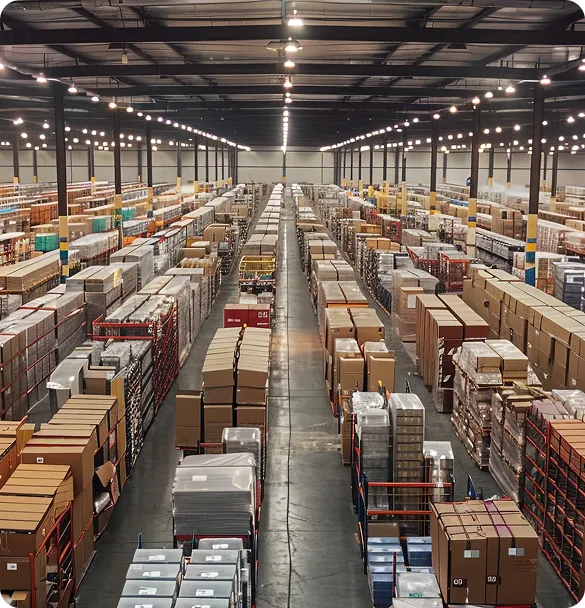
Another important consideration for manufacturers is scalability. A business may begin with relatively simple operational requirements but become more complex as production volumes increase, new facilities are introduced, or product lines expand. Technology should therefore be capable of adapting to changing business needs. Flexible software architecture can allow organizations to introduce additional functionality without completely replacing their existing digital environment. Integration with other business systems can also create a more connected flow of information between manufacturing, finance, procurement, sales, and logistics. This connected approach helps decision-makers understand the wider impact of operational choices instead of viewing each department in isolation.
The food industry presents another area where technology can create significant operational value. Food businesses manage supply chains that can involve farmers, suppliers, processors, manufacturers, warehouses, distributors, retailers, and consumers. Each stage requires careful coordination because product quality, freshness, safety, availability, and delivery timing can directly affect business performance. Food organizations also need to maintain accurate records and respond effectively to changing demand. Digital systems can provide greater visibility across these interconnected activities, helping businesses organize information and coordinate operations more effectively.
Food Supply Chain Management requires particular attention because food products often have specific storage, handling, transportation, and shelf-life requirements. Delays or inaccurate inventory information can result in waste, stock shortages, or difficulties meeting customer demand. Technology can help organizations monitor inventory movement, improve demand planning, coordinate procurement, and maintain better communication with suppliers and logistics partners. When information is available across different stages of the supply chain, businesses can make more informed decisions about purchasing, production, storage, and distribution. This can help create a smoother operational flow while supporting better resource utilization.
Data visibility is one of the most valuable benefits of digital supply chain technology. Organizations can collect information from different operational activities and use it to identify patterns and potential inefficiencies. For example, historical demand information can support better planning, while inventory data can help businesses understand which products require attention. Supplier performance information can also assist organizations in evaluating reliability and identifying opportunities for improvement. When these insights are presented clearly, managers can respond to operational challenges with greater confidence rather than relying entirely on assumptions or incomplete information.
Technology can also contribute to stronger collaboration throughout the supply chain. Manufacturers and food businesses frequently depend on external suppliers, transportation providers, warehouses, and distribution partners. Communication gaps between these participants can create delays and misunderstandings. A connected digital environment can make important information easier to share, helping different parties work from more consistent data. Better collaboration can improve coordination around orders, deliveries, inventory levels, and production requirements, creating a more responsive supply chain.
Security and reliability are equally important as organizations become more dependent on digital systems. Business information can include production data, supplier details, inventory records, customer information, and financial information. Companies therefore need technology solutions that are designed with appropriate access controls, data protection practices, system reliability, and ongoing maintenance in mind. A dependable digital environment can help organizations protect important information while ensuring that employees have access to the data required for their responsibilities.
Digital transformation should also be approached as a continuous process rather than a one-time technology project. Businesses should regularly evaluate their workflows, identify operational challenges, and determine where technology can provide measurable improvements. Employee training and adoption are important parts of this process because even a sophisticated system can deliver limited value if users do not understand how to apply it effectively. Organizations that combine suitable technology with clear processes and effective user adoption are better positioned to achieve lasting operational improvements.
As industrial and food-sector organizations continue to face changing customer expectations, supply chain pressures, and increasing competition, Manufacturing Software Solutions can provide the digital foundation needed for more connected and efficient operations. Similarly, effective Food Supply Chain Management can help organizations improve visibility, coordinate activities, reduce avoidable inefficiencies, and respond more effectively to changing market conditions. Together, these capabilities demonstrate how technology can support businesses in creating more structured, responsive, and data-driven operations.
The future of business technology will increasingly depend on connected systems, intelligent data analysis, automation, and adaptable digital platforms. Organizations that invest in technology with a clear understanding of their operational objectives can build processes that are easier to monitor, manage, and improve. Lynqcore Solutions can support this broader digital transformation journey by helping businesses explore technology-driven approaches suited to their operational requirements. With the right combination of software, data, processes, and people, businesses can create stronger operational foundations and remain prepared for the opportunities and challenges of an increasingly digital marketplace.
Comments
Post a Comment